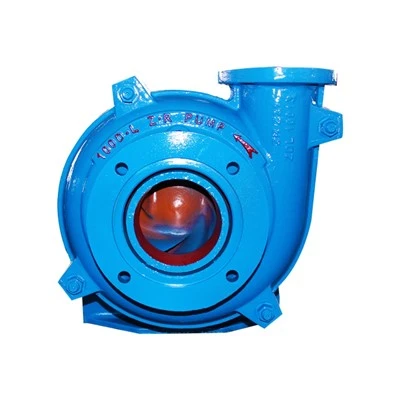
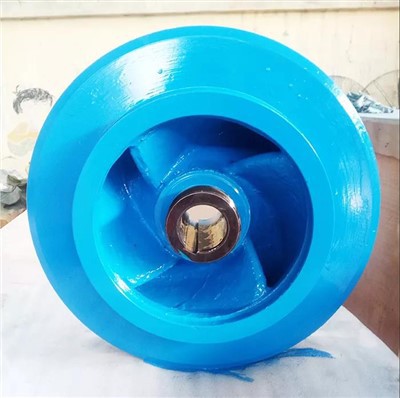
A slurry pump is an industrial pump specifically designed for transporting slurries containing solid particles (such as ore slurry, mud, ash, etc.). Its core function is to efficiently and stably handle highly abrasive, high-concentration mixed media, playing an irreplaceable role in mining, metallurgy, power generation, coal mining, chemical engineering, and other fields.
I. Basic Functions of Slurry Pumps
The primary function of a slurry pump is to transport slurries containing solid particles from low to high locations or over long distances to a designated location. Unlike ordinary water pumps, slurry pumps are designed to withstand the impact and abrasion of solid particles. Key components such as the impeller and pump casing are typically made of highly wear-resistant materials (such as rubber and alloy steel) to ensure long-term stable operation even under harsh operating conditions.
II. The Core Role of Slurry Pumps
1.Slurry Transportation in the Mining Industry
During the mineral processing process, ore is crushed and ground to form a highly concentrated slurry. Slurry pumps are responsible for transporting this slurry from the ore bin to the flotation machine, thickening tank, or dewatering equipment, making them an indispensable part of the mineral processing process.
2.Ash Treatment in the Metallurgical and Power Industries
Coal-fired power plants and metallurgical plants generate large amounts of boiler bottom ash and metallurgical waste slag. Slurry pumps are used to transport slurry from wet deslagging systems to the slag bin or processing equipment, ensuring production continuity and environmental compliance.
3.Slurry Transportation in the Coal and Chemical Industries
In coal washing and chemical production, slurry pumps are used to transport coal slime, chemical slurries, and other materials. Their wear resistance enables them to handle highly concentrated and corrosive media, improving production efficiency and reducing maintenance costs.
III. Unique Advantages of Slurry Pumps
•High Wear Resistance: Made of special materials (such as A05 rubber and Cr27 alloy) for extended service life.
•Suitable for high-concentration slurries: Capable of conveying slurries with solids contents exceeding 60%, meeting the needs of heavy industry.
•Efficient and stable: Optimized hydraulic design ensures low energy consumption and high-lift conveying.
IV. Future Development Trends
With advances in industrial technology, slurry pumps are developing towards intelligent, energy-efficient, and wear-resistant technologies. For example, variable frequency control technology is being used to optimize energy consumption, nano-coatings are being used to enhance wear resistance, and intelligent monitoring systems are being used to predict failures, further enhancing operational reliability.
In summary, as key equipment for industrial slurry conveying, slurry pumps not only improve production efficiency but also play a vital role in ensuring production safety and reducing maintenance costs. As demand for efficient conveying grows across various industries, technological upgrades in slurry pumps will continue to drive progress in the industrial sector.